Pressure Reducing
Pressure Sustaining / Pressure Relief
Flow Control valves
Float Valves - Level Control
Electrically Actuated Valves
Pressure Modulation - Remote Control
Altitude Valves - Level Control
Burst Control Valves
Pump Control
CLA-VAL "HYTROL" Main Valve
Valve Controllers and Data Loggers
Air Valves
Choosing the right Textile Lamination Machine in 2026 requires more than comparing speed, price, and attractive specifications. A machine may promise 30 meters per minute, yet unstable tension can create wrinkles, weak bonding, or uneven edges. The real test appears on the production floor, beside the roll stand, heated rollers, and finished fabric.
Dr. Behnam Pourdeyhimi, a respected textile materials researcher, offers a useful principle: “Performance must be measured in the finished material, not just in the machine.” This idea should guide every purchasing decision. Buyers need to examine substrate compatibility, adhesive application, heating accuracy, pressure control, web width, and cooling performance. Energy consumption also matters. So does operator training.
This guide evaluates the 2026 best Textile Lamination Machine options through practical and technical criteria. It considers textile manufacturers, nonwoven producers, protective fabric suppliers, and flexible material converters. The strongest machine is not always the fastest one. Sometimes, a slower system delivers cleaner bonding and fewer rejected rolls.
Small details matter.
Check tension recovery after a roll change. Inspect adhesive coating under real production conditions. Ask whether spare parts arrive quickly. Review service records, not only brochures. A machine can look impressive during a demonstration, but daily maintenance may reveal its weaknesses. No buying guide can remove every uncertainty. However, careful testing, transparent supplier communication, and measurable quality targets can reduce expensive mistakes. That is where informed purchasing begins.
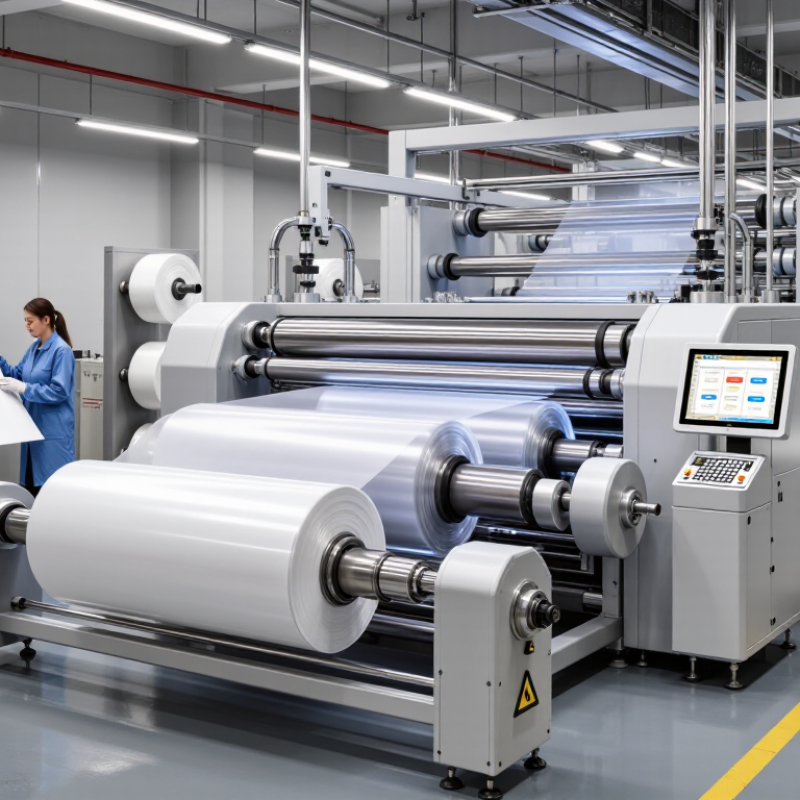
A textile lamination machine bonds fabric with another layer, such as film, foam, foil, or nonwoven material. It creates a combined textile with improved water resistance, insulation, strength, or surface protection. The machine usually includes unwinding units, tension controls, heating rollers, a laminating nip, cooling rollers, and a rewinding system.
During operation, the fabric and bonding layer travel at a controlled speed. Heat softens the adhesive or thermoplastic surface. Pressure then presses both materials together. Cooling helps stabilize the finished laminate. Some machines apply liquid adhesive before pressing, while others use pre-coated films. Temperature, pressure, speed, and tension must remain balanced. A small setting error can cause wrinkles, weak bonding, or adhesive marks. The first trial is rarely perfect.
Tips: Test the actual fabric before purchasing. Check its thickness, stretch, heat sensitivity, and surface texture. Ask for production samples at your expected speed. Review coating width, temperature range, roller design, and cleaning access. Operators should also inspect alignment and bond strength during long runs. A simple peel test can reveal problems early. Do not judge performance by speed alone. Stable tension often matters more.
Choosing a textile lamination machine starts with the material, not the advertised output speed. Textile Exchange’s Materials Market Report 2024 recorded global fiber production at 124 million tonnes in 2023. That scale reflects highly different fabrics, finishes, and bonding needs.
For breathable jackets, hot-melt film laminators suit TPU, PU, and membrane constructions. They offer accurate temperature control and limited adhesive spread. Use low-tension rollers for delicate knits. Not every fabric agrees.
Flame lamination works better for foam-backed fleece, insulation, and automotive padding. It bonds through controlled heat and can cover wide rolls quickly. However, excessive heat may distort synthetic fibers or weaken surface coatings. A short trial is essential.
For medical textiles and protective garments, solvent-free PUR or adhesive-film systems provide cleaner, controlled bonding. They fit narrow tolerance requirements and multi-layer assemblies. Heavy upholstery and interior fabrics may need knife-over-roll coating followed by heated calender rollers. Grand View Research estimated the global technical textiles market at about USD 225.99 billion in 2023, with projected growth near 6.2% annually through 2030. That expansion increases demand for dependable, application-specific equipment.
In production trials, buyers often focus too much on speed. Peel strength, hydrostatic pressure, breathability, wash durability, and adhesive migration deserve equal attention. Perfect settings are rare. Leave room for adjustment. A machine that handles one fabric beautifully may perform poorly on another. Record temperature, pressure, line speed, and curing time during every material test.
When comparing textile lamination machines, start with measurable process control, not advertised speed. Textile Exchange’s 2024 Materials Market Report states that global fiber production reached about 124 million tonnes in 2023. That scale increases pressure on manufacturers to reduce waste, defects, and rework. A suitable machine should offer stable web tension, adjustable nip pressure, and accurate adhesive dosing. These controls protect fabric stretch and prevent bubbles, edge lifting, and uneven bonding.
Speed is important, but only with consistent results. Check the usable working width, line speed under real production conditions, and temperature uniformity across the heating zone. A machine rated at 30 meters per minute may run slower with heavy fabrics or water-based adhesive. Ask for trial data. Energy consumption also matters. The International Energy Agency reports that industrial motors account for roughly 30% of global electricity use, making efficient drives and heating systems practical purchasing criteria. Small savings become significant during continuous operation.
Inspect the machine’s sensor system, tension feedback, cleaning access, and changeover time. Digital traceability helps operators compare pressure, temperature, and speed during each batch. Smithers’ technical outlooks on nonwovens repeatedly emphasize automation and process consistency as growth drivers. Still, published figures can look better than factory experience. I would test uneven rolls, elastic fabrics, and low-temperature bonding before approving a purchase. One overlooked detail remains maintenance access. A difficult-to-clean coating head can quietly reduce output every week.
| Technical Specification | Hot-Melt Powder Lamination | Film Lamination | Flame Lamination | Water-Based Adhesive Lamination |
|---|---|---|---|---|
| Typical application | Apparel interlinings, automotive textiles, protective fabrics, technical laminates | Rainwear, mattress covers, medical textiles, breathable and barrier fabrics | Foam-backed upholstery, furniture fabrics, automotive seat materials | Home textiles, nonwovens, hygiene materials, low-temperature fabric assemblies |
| Usable lamination width | 1,600–3,200 mm | 1,600–3,200 mm | 1,600–2,400 mm | 1,600–3,200 mm |
| Typical working speed | 10–35 m/min | 15–50 m/min | 20–60 m/min | 10–40 m/min |
| Compatible substrate weight | 30–600 g/m² | 30–800 g/m² | 80–1,200 g/m², including foam assemblies | 30–500 g/m² |
| Adhesive or bonding medium | Thermoplastic adhesive powder | Thermoplastic adhesive film or web | Direct flame activation of polyurethane foam | Water-based polymer adhesive |
| Typical bonding temperature | 100–180 °C, depending on polymer type | 90–170 °C, depending on film chemistry | Foam surface activation; controlled by flame intensity and line speed | 80–150 °C drying and curing zone |
| Heating system | Electric infrared, hot-air, oil-heated, or heated calender | Electric infrared, hot-air oven, or heated roller | Gas burner with flame-control and exhaust system | Hot-air circulation or multi-zone drying oven |
| Temperature control accuracy | Typically ±2–5 °C per controlled zone | Typically ±2–5 °C per controlled zone | Typically monitored through burner, airflow, and line-speed controls | Typically ±2–5 °C per drying zone |
| Typical nip pressure range | 0.2–0.8 MPa | 0.2–1.0 MPa | 0.1–0.6 MPa | 0.2–0.8 MPa |
| Adhesive application control | Powder scatterer with adjustable coating weight, commonly 5–80 g/m² | Film unwinder with edge guiding and tension control | Foam thickness, flame gap, gas flow, and line speed | Metering roller, gravure roller, spray, or knife coating |
| Maximum roll diameter | 800–1,200 mm | 800–1,200 mm | 800–1,000 mm | 800–1,200 mm |
| Electrical connected load | 60–180 kW | 50–160 kW | 25–90 kW, excluding gas supply | 80–220 kW |
| Compressed-air requirement | 6–8 bar; approximately 0.3–1.0 m³/min | 6–8 bar; approximately 0.2–0.8 m³/min | 6–8 bar; approximately 0.3–1.0 m³/min | 6–8 bar; approximately 0.3–1.0 m³/min |
| Cooling method | Water-cooled or air-cooled calender and cooling rollers | Water-cooled or air-cooled bonding rollers | Air cooling and controlled cooling rollers | Air cooling or water-cooled rollers |
| Tension-control features | Load-cell dancer, automatic edge alignment, variable-frequency drives | Independent unwind tension, edge guide, dancer roller, servo synchronization | Fabric and foam tension control with synchronized roller drives | Unwind and rewind tension control with edge alignment |
| Expected bonding uniformity | High when powder distribution and temperature are correctly calibrated | Very high with consistent film thickness and web tension | High, but strongly affected by foam surface condition and flame settings | High after correct viscosity, coating weight, and drying control |
| Main advantages | Flexible coating weight, good pattern control, suitable for varied textile constructions | Clean process, precise adhesive thickness, strong barrier performance | Fast bonding, no separate adhesive film or powder handling, suitable for foam composites | Low-solvent or solvent-free process, adaptable coating methods, soft hand feel |
| Main limitations | Requires powder recovery, dust control, and accurate melting conditions | Film cost, roll-change management, and potential stiffness at high coating weights | Requires gas safety controls, exhaust ventilation, and compatible foam substrates | Longer drying zones and sensitivity to humidity, viscosity, and residual moisture |
| Recommended quality checks | Peel strength, coating-weight distribution, melt temperature, delamination rate | Peel strength, film thickness, pinholes, web alignment, seam continuity | Peel strength, foam damage, flame profile, surface activation, odor | Peel strength, dry-bond performance, moisture content, coating weight, curing level |
| Best suited production scale | Medium to high volume with multiple product specifications | Medium to high volume requiring repeatable barrier or film-based performance | Continuous high-volume foam and upholstery production | Small to high volume, depending on drying capacity and adhesive formulation |
2026 Best Textile Lamination Machine Buying Guide
How to Evaluate Production Capacity, Quality, Safety, and Energy Efficiency?
Production capacity should be measured under real operating conditions, not catalog speed alone. Ask for sustained output using your actual fabric width, coating weight, and adhesive type. During a factory trial, record meters per hour, changeover time, web tension, and unplanned stops. A machine rated at 80 meters per minute may deliver far less after warming, cleaning, and roll replacement. That gap matters.
Quality depends on control, repeatability, and inspection. Check bonding strength across the roll, not only at its center. Examine edge alignment, wrinkles, bubbles, coating uniformity, and surface temperature. Request test samples from different production shifts. Keep the settings and test results. This creates useful evidence. Still, one successful trial proves little. Humidity, operator skill, and fabric variation can expose weaknesses later.
Safety evaluation should include guarding, emergency stops, interlocks, heated zones, and accessible maintenance points. Ask how operators isolate power before cleaning or removing jammed material. Confirm ventilation for heat and adhesive emissions, according to applicable local requirements. For energy efficiency, measure electricity and compressed-air use during startup, production, standby, and shutdown. Look for insulated heating sections, automatic temperature control, and low-loss pneumatic components. An energy display is helpful, but independent meter readings are more trustworthy. Allow space for training and maintenance; a crowded machine often creates avoidable risks.
Choosing a textile lamination machine starts with the supplier, not the catalog price. Request factory experience, engineering qualifications, installation records, and customer references from similar materials. A reliable supplier should explain adhesive systems, coating width, heating control, line speed, and maintenance needs clearly. Ask for production videos and measurable results, not polished promises.
Estimate the full cost before signing. Include the machine, shipping, installation, operator training, energy use, spare rollers, replacement heaters, and annual maintenance. Ask for a written quotation with delivery dates and warranty conditions. Some estimates will be wrong. Electricity consumption can rise when fabrics require higher drying temperatures. I learned this matters after comparing planned costs with actual factory use.
Tips: Send your real fabric samples for a performance trial. Record line speed, bonding strength, coating uniformity, temperature stability, and waste percentage. Request test data with dates, instruments, and operating settings. During factory acceptance testing, inspect emergency controls, roller alignment, tension response, and cleaning access. A short trial is useful, but it can hide long-run problems. Run several hours with changing fabric rolls when possible. Also ask how quickly the supplier provides technical support and critical spare parts. Verify every claim through samples, records, and direct conversations with existing users.
CLA-VAL UK Limited
Dainton House
Goods Station Road
Tunbridge Wells
Kent, TN1 2DR
© 2025 CLA-VAL UK | site map | Terms and Conditions of Sale and Warranty | Privacy policy